
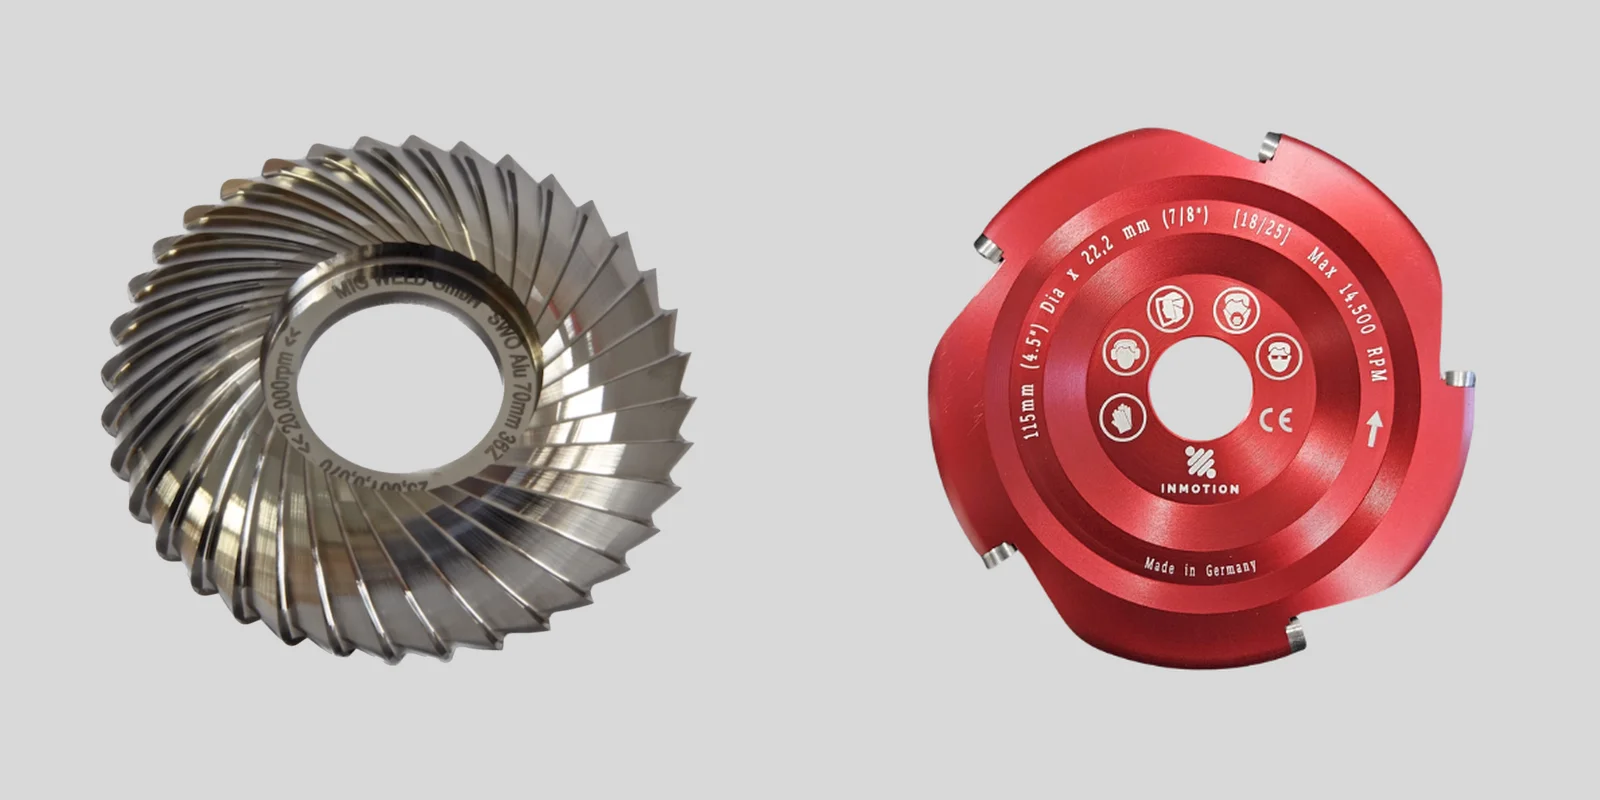
Two carbide discs now compete for aluminum weld prep on an angle grinder. One is a solid-carbide milling disc that you resharpen. The other is a disc body with replaceable carbide inserts that you swap in the shop.
We sell both, so we have no reason to tilt the comparison. Here’s how they differ and who should buy which.
What both carbide discs do better than abrasives
Both designs cut metal with carbide edges, where abrasives wear it away with grit. That changes three things on aluminum, and all three hold for either concept.
No embedded grit. Aluminum is soft, and abrasive wheels can leave foreign material in the surface. Fronius, a welding equipment maker, tells fabricators to “avoid consumables such as a grinding wheel or sandpaper that can embed foreign material into the base metal.” MSC Direct’s aluminum guide says porosity can occur when contaminants from abrasive products release from the wheel and contaminate weld surfaces. A carbide edge has no resin-bonded grit to leave behind.
Chips, not fine dust. OSHA’s combustible dust guidance lists aluminum among the metals that can be explosible in dust form, even though a block of aluminum won’t burn. Grinding makes that fine dust. Milling makes chips you can sweep up. That cuts the airborne dust. It doesn’t replace housekeeping, and shops handling combustible metal dust should still work to NFPA 484, the standard for combustible metals.
No loading. Heat and friction make aluminum stick to an abrasive until, as MSC puts it, “this loading or clogging of material eventually prevents the abrasive from cutting.” A cutting edge clears chips instead.
If you’re still on flap discs, our longer piece on why grinding discs fail on aluminum covers the mechanics. The rest of this article is about choosing between the two carbide options.
The two concepts
Solid-carbide milling disc. One piece of carbide, made in Germany to EN 847-1 and supplied through MIGAL.CO. It runs 300 to 500 hours per cycle and gets resharpened 5 to 7 times, for up to 4,000 hours of total life. It comes single-sided, double-sided or as a Doubleworker. Inmotion coordinates the resharpening. Our product page is /milling-disc/.
Indexable-insert disc. A reusable disc body with five replaceable carbide inserts. When the edges dull, you fit new inserts yourself. Inmotion’s US distribution partner for this design is Heavy Hitters, which sells the AluCarver milling disc. In their shop it carries their own brand name, Duz-AL 4-1/2” Non-Ferrous Milling Disc, so look for that. The listing is for a 4-1/2” disc with a 10 mm cutting width, for non-ferrous metals only, and names root weld opening among its uses alongside chamfering and seam trimming.
What happens when the edge goes dull
This is the real difference in daily work.
- 1Disc dulls After 300 to 500 hours the cut slows and the finish gets worse.
- 2Ship it out The disc goes to Inmotion, which coordinates resharpening through the manufacturer.
- 3Work continues on a second disc Shops that can't stop weld prep keep a second disc to bridge the gap. That is extra capital on the shelf.
- 4Disc comes back Resharpened and ready for another cycle. Five to seven cycles per disc.
With the insert disc, there is no loop. You reorder inserts, swap them at the bench and keep going. No shipping, no second disc waiting.
That convenience is the case for the insert design. The case for the solid disc is in the table below.
Side by side
| Solid-carbide milling disc | Indexable-insert disc | |
|---|---|---|
| Upfront cost | At least roughly twice the insert disc at current US list prices | Lower |
| When the edge dulls | Resharpen: send the disc out, get it back | Replace the inserts on site |
| Downtime | Disc is away during resharpening; plan a second disc | Only the time to swap inserts |
| What you reorder | Nothing until the disc is worn out after 5 to 7 resharpenings | Inserts |
| Aluminum | Yes, 8,500 to 15,300 rpm | Yes |
| Steel | Yes, with steel-specific geometry at 1,800 to 3,200 rpm | No, listed as not for ferrous metals |
| Disc geometries | Single-sided, double-sided, Doubleworker | 4-1/2" disc, 10 mm cutting width |
| Chips vs dust | Chips | Chips |
| Best for | Steel and mixed materials, double-sided root work, longest total life | Aluminum-only prep including root opening, lower entry cost, no send-out cycle |
We left out insert pricing and edge life on purpose. We don’t have verified numbers for either, and we won’t guess. Ask Heavy Hitters before you budget.
Aluminum is the main use case. Steel is possible.
Most weld prep we see is aluminum: bevels, V-grooves, seam trimming, cleaning up cast flash before re-welding. Both discs fit.
Steel changes the picture. A solid-carbide disc with steel geometry works, but it runs at 1,800 to 3,200 rpm rather than aluminum’s 8,500 to 15,300, and it’s a different disc. The economics differ too, so run the numbers for your volume. The insert disc isn’t an option here, since its listing says it isn’t for ferrous metals.
Match the disc to the material
Don’t run an aluminum disc on steel, or the reverse. Tooth geometry and rpm are set per material. For the solid-carbide disc, the grinder baseline is at least 1,500 W and 12,000+ rpm.
Which one fits your shop
Teal = Decisive
If your situation is mixed, the material usually decides. Steel, stainless and titanium point to the solid disc. Aluminum only comes down to cost model: a higher price up front with a long life, or a lower price and a bench-side swap.
Next step
Featured Hardware
Rotary Milling Disc
Steel, double-sided discs or the longest total life? Tell us your material and the work.
Request a milling disc quote →Aluminum only, lower upfront cost, no send-out cycle?
See the insert disc at Heavy Hitters →Frequently Asked Questions
What is a carbide milling disc?
A disc for an angle grinder that cuts metal with carbide teeth instead of grinding it with abrasive grit. It removes material as chips, so there is no abrasive to embed in the part. Two designs exist: a solid-carbide disc that gets resharpened, and a disc body that carries replaceable carbide inserts.
Can a milling disc be resharpened?
A solid-carbide milling disc can. Inmotion's disc runs 300 to 500 hours per cycle and can be resharpened 5 to 7 times, for up to 4,000 hours of total life. It goes out for resharpening and comes back. An insert disc isn't resharpened. You replace the inserts.
Can you use a milling disc on steel?
Yes, with a solid-carbide disc that has steel-specific tooth geometry, run at 1,800 to 3,200 rpm. Aluminum discs run at 8,500 to 15,300 rpm. The insert disc we point readers to is listed for non-ferrous metals only.
Is a milling disc better than a flap disc on aluminum?
For weld prep, usually yes. A milling disc cuts chips and leaves no abrasive residue. A flap disc can embed grit in soft aluminum and load up with smeared metal, and grinding throws fine aluminum dust into the air.
What angle grinder do I need for a solid-carbide milling disc?
An electric or pneumatic angle grinder rated for at least 1,500 W and 12,000+ rpm.